Attention and Information Sampling During Active Cutting
That financial reality creates a cognitive environment foreign to consumer electronics. The machinist is not staring at your interface with full attention. They are monitoring chip formation through a safety window, listening for spindle chatter that indicates tool wear, and mentally calculating the next workpiece setup while the current cycle runs. The HMI competes with coolant spray, alarm beeps, and the physical vibration of a 12,000 RPM cutter engaging alloy steel. Experienced operators sample displays every 15 to 30 seconds while focusing on the physical process. Information must be glanceable during active cutting, not just legible during setup. This means the primary display hierarchy cannot follow desktop software conventions where depth of navigation indicates sophistication. Every second spent drilling through menu levels is a second the operator is not watching the cut, and in unattended operation, a confused operator is more dangerous than a malicious one.

Photo by Sergey Sergeev on Pexels
Hardware Ergonomics and Glove-to-Glass Friction
This peripheral attention requirement drives every decision about physical CNC panel design. The operator stands at a 15-degree angle to the screen, often wearing safety glasses that polarize light and nitrile or leather gloves that transform precise capacitive touch into frustrated stabbing. Ambient lighting ranges from dim corners to welding glare, requiring 1000+ nits brightness. Coolant mist coats screens within hours, creating a film that obscures touch registration. Metal chips conduct electricity and scratch glass. A control panel designed in a clean office assumes a user who sits, sees clearly, and touches delicately. The shop floor punishes each of these assumptions. Physical buttons provide tactile confirmation that an input registered; rotary jog wheels allow precise axis movement without looking at the control. ISO 7000 symbols must indicate function without requiring text parsing. Removing these hardware elements for aesthetic minimalism eliminates sensory feedback loops that prevent crashes and increases training time for new operators, a hidden cost that compounds in high-turnover shops.
Hybrid Controls Over Pure Touchscreen in Machine Tool Interfaces
This reality explains why the industry transition to pure touchscreen interfaces has produced as many failures as efficiencies. FANUC and Siemens, the two dominant manufacturers of CNC operator interfaces, have learned through decades of shop-floor deployment that touch alone cannot reliably handle coolant and machine vibration. FANUC’s latest iHMI retains membrane keys and physical jog wheels alongside its glass display specifically because unintended inputs from vibration can jog a spindle into a fixture before the operator notices, a costly crash. Siemens’ SINUMERIK ONE ships with hardware rated for IP65 oil resistance because phantom touches create ghost commands in unattended operation. Requiring a machinist wearing leather work gloves to pinch-zoom a screen creates production downtime while they remove hand protection to interact with the machine. The viable architecture is hybrid: touch for data entry and visualization, physical controls for motion and emergency stops. This redundancy is not design conservatism; it is the only way to maintain safety when the operator cannot always watch the screen.
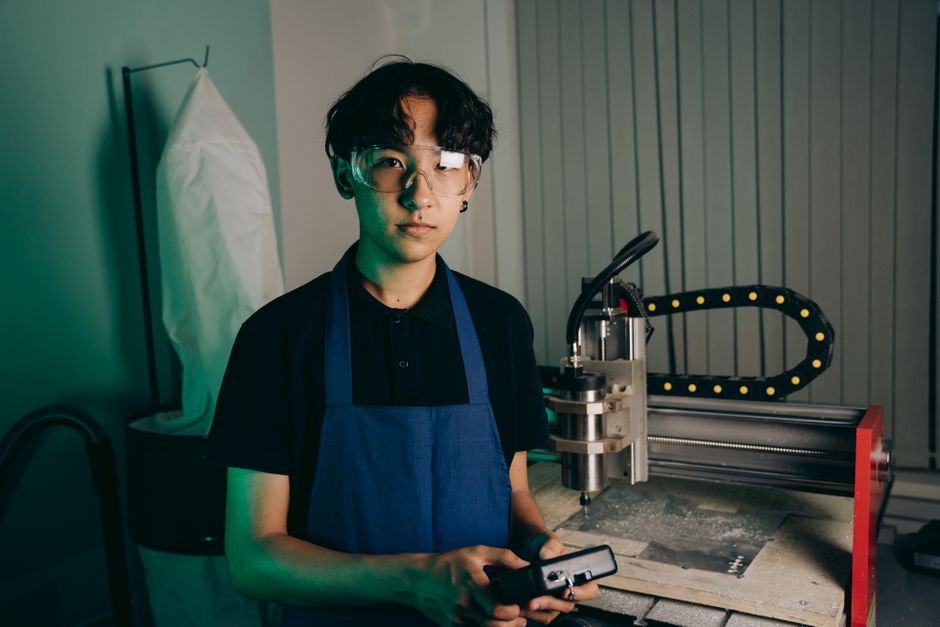
Photo by Mikhail Nilov on Pexels
Mode Status and Persistent Information Architecture
If the input layer must be hybrid, the information architecture must match the machinist’s mental model of machine states. CNC operation moves between distinct modes (Manual, MDI, Auto, Edit), each with different permission levels and risk profiles. The interface must make mode status impossible to miss, not merely indicated. A green bar at the top is insufficient when the operator is looking at the tool tip, not the screen. Critical parameters like feed rate override, spindle speed, and axis position must remain visible regardless of which submenu is active. Color coding follows industrial standards: red for emergency, yellow for warning, never red for active cutting. This is not discoverability; it is persistent ambient awareness. Unlike consumer software where features can be buried in settings, machine tool UX engineering requires that safety-critical functions occupy fixed spatial locations that muscle memory maps after weeks of operation. Changing these locations between software versions breaks operator fluency and increases error rates.